
Laminate bubbles are the most common defect in solar module encapsulation. This blog breaks down the two main bubble types
Quick answer: Not every bubble in a laminated module comes from the encapsulant, and treating them all as a material problem leads to the wrong fix. Some bubbles originate in the vacuum system: if the chamber does not evacuate fast enough or the pump set cannot hold the required vacuum through the cycle, air remains trapped in the stack and shows up as voids after crosslinking. The distinction matters because the two causes have entirely different remedies. A material cause points to encapsulant moisture content, storage or the crosslinking window. A vacuum cause points to pump capacity, seal condition, leak rate or the evacuation profile. The pump configuration and the EVA thermal window are what set the deadline for removing the air before the encapsulant starts to gel.
PV Module Manufacturing · by Jerry, Ooitech
Introduction
Some bubble defects originate in the vacuum system rather than the encapsulant; the pump configurations and the pumping deadline are explained in laminator vacuum pumps, the EVA window and how the pump set is configured.
Every time a bubble shows up in a solar module, people rush to blame the EVA/EPE film. It's not that simple.
In PV module encapsulation, laminate bubbles are the most common and the most stubbornly recurring quality defect. Most people in the industry hold a fixed belief that laminate bubbles are all caused by EVA/EPE encapsulant quality problems. That's not true. Encapsulant defects are only one of many causes. Raw material flaws, abnormal lamination equipment, human operation errors, and a workshop environment out of control can all trigger different types of laminate bubbles.
Bubbles look like a surface cosmetic flaw, but they keep affecting the module's power output, long-term stability and service life. They are one of the core hidden causes behind outdoor degradation, delamination and failure. This blog looks at bubble classification, root causes and performance damage from multiple angles, giving you a precise basis for process optimization and defect traceability.
Types of PV Module Laminate Bubbles and Their Causes
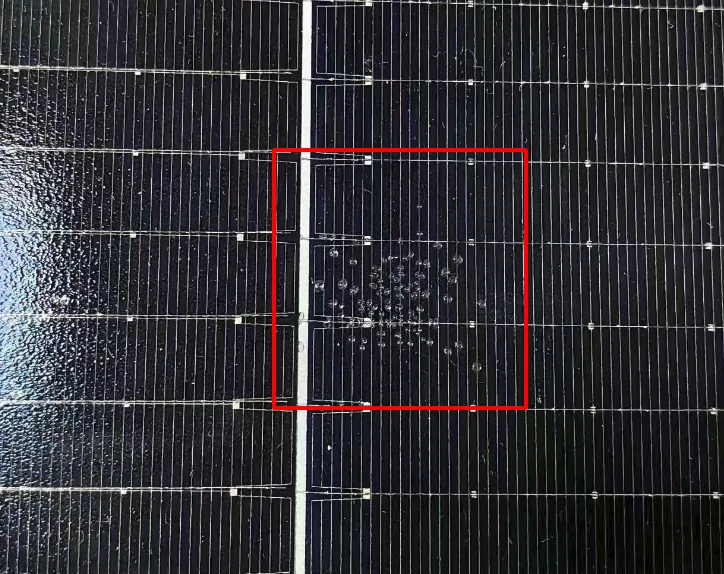
Based on bubble shape, distribution and formation mechanism, laminate bubbles fall into two core categories.
Residual Bubbles
These mainly appear in the cell gaps, string spacing, module edges and four corners. They show up as dense small bubbles, strip-shaped bubbles or snowflake-shaped bubbles. The core cause is that interlayer air is not fully expelled during lamination and vacuum degassing is incomplete. They are physical residual bubbles, mostly tied to equipment parameters, operation process and layup process, with material defects making up a very small share. These bubbles are small at first, highly hidden, and may still pass each factory's quality standard. In mass production they are easily overlooked, but the risk of later expansion is very high.
Detailed analysis:
Outgassing Bubbles
These mostly appear on the cell surface, around the ribbon and in local module areas, mainly as single large bubbles or locally dense bubbles. The core cause is moisture inside the materials (film, glass, ribbon, cells), volatiles (flux, etc.), or residual impurities in auxiliary materials. During high-temperature lamination, moisture and small-molecule impurities vaporize under heat and the gas can't escape, so it gathers into bubbles. This is mainly tied to raw material quality, auxiliary material control and material pretreatment. So there are many material-side causes too — don't be so sure it's the film every time a bubble appears. Detailed analysis:
Beyond Equipment, Process and Materials: Operators and Environment
Besides equipment, process and materials, human operation errors and workshop environment can also cause bubble defects.
The Damage Goes Beyond Looks: Reliability and Safety Too
Laminate bubbles affect more than the module's appearance — they hit reliability and safety.
Appearance: Direct Reject, Lower Yield
Bubbles break the flat, uniform look of the module surface and form a visible cosmetic defect. They are a core failure item in the first inspection. By PV module inspection standards, when bubble count, size or position exceeds the spec, the module is directly judged as cosmetic reject and can't be shipped. That means scrap and rework loss, and lower line yield and efficiency. Irregular bubbles also make surface light transmission uneven, hurting product consistency and market perception.
Performance: Lower Output, Faster Power Loss
A bubble is essentially a sealed cavity between layers, holding residual air, moisture or outgassed gas, and it changes the module's internal optical structure. On one hand, the bubble area refracts, reflects and scatters light, cutting the effective light-receiving area of the cell and lowering photoelectric conversion efficiency — the initial power comes out low. On the other hand, in the bubble area the encapsulant can't bond tightly with cell, glass and backsheet, so heat conduction drops sharply, local heat builds up during operation and creates hot-spot risk. Over long-term running, hot spots keep scorching the cells, causing microcracks and accelerated degradation, so annual power loss far exceeds the standard value and the effective generating life shrinks a lot.
Reliability: Encapsulation Failure and Safety Hazards
This is the most core and deadly damage from laminate bubbles. Modules sit outdoors for years through heat, cold, rain, snow, wind, sand and UV. Day-night and seasonal temperature swings make the gas inside the bubble expand and contract over and over, constantly pulling on the interlayer interface. Under long-term stress, tiny bubbles gradually grow and merge, finally causing delamination and peeling between the film and the glass, cells and backsheet. Once delaminated, the module's seal completely fails, and moisture, damp and corrosive media keep seeping in, leading to ribbon oxidation, cell corrosion, PID degradation, mold and blackening. In severe cases it causes insulation drop, leakage or short circuit — safety faults that hurt plant generation stability, drive up O&M cost, and bring plant safety accident risk, badly cutting the 25-year service life guarantee.
Ooitech's View
Bubbles rarely come from one single cause, and that's exactly why treating them as "an encapsulant problem" burns time chasing the wrong batch of film. From the lines we deliver, the pattern holds: residual bubbles trace back to vacuum, pressure and layup, while outgassing bubbles trace back to moisture and flux control — so a stable laminator recipe plus disciplined pretreatment and 5S usually fixes more than swapping film ever will. If you want to see how proper degassing, holding pressure and layup alignment play out on a real production line, the walkthroughs on our YouTube channel www.youtube.com/ooitech are worth a look. Get the process right first, then the film gets a fair trial.